


Key points of selection, assembly and spot solid welding of aluminum and aluminum alloy Welding materials
Release time:
2022-11-01
【Summary Description】 Choice of Welding materials In principle, aluminum and aluminum alloy welding wires or strips with the same composition as the base metal should be selected. Argon purity> 99.95%, try to use large diameter welding wire. Aluminum-magnesium-aluminum alloy arc welding usually recommend the use of CB-AMr2, CB-AMr3, CB-AMr6, CB- AMr61, CB-AMr63, 1557 and 1577 electrodes, and aluminum-copper-aluminum alloy recommend use 01201 and 01217 electrodes. Assembly and spot welding Due to the fast heat conduction of aluminum and aluminum alloy pipes, the crystallization is fast in the molten pool, the weld length of 10-15mm is easy to locate, and there is no gap and blunt edge, so the large residual stress caused by strong exercise after welding should be avoided. The welding positions are at 7 o'clock, 9 o'clock and 12 o'clock of the pipeline. Positioning welds are often reserved as formal welds, so problems should be dealt with in time. Before welding, remove the black powder and oxide film on the tack welding surface, and make both ends smooth. Welding parts do not require preheating. Before welding, try welding on the test plate to confirm that there is no air hole before formal welding. Using high-frequency arc, the starting point should be about 20mm above the center line, and it should be stationary for about 2-3 seconds. Then, under the condition of ensuring the penetration depth, the high current rapid welding is adopted. The welding wire shall not swing and the end of the welding wire shall not leave the argon protection zone. If leaving the argon protection zone, the end of the wire should be cut off. The angle between the wire and the weld surface shall be 15 degrees right angle. The angle between the torch and the weld surface should be maintained between 80 degrees and 90 degrees. In order to increase the argon protection area and enhance the protection effect, the large-diameter ceramic nozzle of the welding gun can be used to increase the argon flow of the welding gun. When there is spatter on the nozzle that significantly impedes the flow of argon. The spatter must be removed or the nozzle replaced. When the tungsten electrode is contaminated and irregularly shaped, it must be trimmed or replaced. The tungsten should not protrude from the nozzle. The control of welding temperature is mainly the control of welding speed and welding current. The test results show that high current rapid welding can effectively prevent the generation of pores. This is mainly due to the fast penetration of the weld during the welding process, the short heating time of the molten metal, and the less chance of absorbing gas. When closing the arc, pay attention to fill the arc pit, reduce the molten pool, and avoid shrinkage. The connection of the end point shall be welded for 20~30mm, and the air shall be stopped for 6 seconds after the arc is stopped. When rotating aluminum and aluminum alloy pipe butt welding, the welding torch should be in a slightly uphill welding position. This facilitates penetration. Thick wall tube bottom welded. Wire cannot be added. However, the welding wire shall be added in the subsequent welding layer.
Welding materials的选择
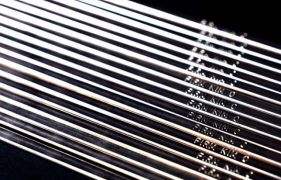
In principle, aluminum and aluminum alloy welding wires or strips with the same composition as the base metal should be selected. Argon purity> 99.95%, try to use large diameter welding wire. Aluminum-magnesium-aluminum alloy arc welding usually recommend the use of CB-AMr2, CB-AMr3, CB-AMr6, CB- AMr61, CB-AMr63, 1557 and 1577 electrodes, and aluminum-copper-aluminum alloy recommend use 01201 and 01217 electrodes.
Assembly and spot welding
Due to the fast heat conduction of aluminum and aluminum alloy pipes, the crystallization is fast in the molten pool, the weld length of 10-15mm is easy to locate, and there is no gap and blunt edge, so the large residual stress caused by strong exercise after welding should be avoided. The welding positions are at 7 o'clock, 9 o'clock and 12 o'clock of the pipeline. Positioning welds are often reserved as formal welds, so problems should be dealt with in time. Before welding, remove the black powder and oxide film on the tack welding surface, and make both ends smooth. Welding parts do not require preheating. Before welding, try welding on the test plate to confirm that there is no air hole before formal welding. Using high-frequency arc, the starting point should be about 20mm above the center line, and it should be stationary for about 2-3 seconds. Then, under the condition of ensuring the penetration depth, the high current rapid welding is adopted. The welding wire shall not swing and the end of the welding wire shall not leave the argon protection zone.
If leaving the argon protection zone, the end of the wire should be cut off. The angle between the wire and the weld surface shall be 15 degrees right angle. The angle between the torch and the weld surface should be maintained between 80 degrees and 90 degrees. In order to increase the argon protection area and enhance the protection effect, the large-diameter ceramic nozzle of the welding gun can be used to increase the argon flow of the welding gun. When there is spatter on the nozzle that significantly impedes the flow of argon. The spatter must be removed or the nozzle replaced. When the tungsten electrode is contaminated and irregularly shaped, it must be trimmed or replaced. The tungsten should not protrude from the nozzle. The control of welding temperature is mainly the control of welding speed and welding current. The test results show that high current rapid welding can effectively prevent the generation of pores.
This is mainly due to the fast penetration of the weld during the welding process, the short heating time of the molten metal, and the less chance of absorbing gas. When closing the arc, pay attention to fill the arc pit, reduce the molten pool, and avoid shrinkage. The connection of the end point shall be welded for 20~30mm, and the air shall be stopped for 6 seconds after the arc is stopped. When rotating aluminum and aluminum alloy pipe butt welding, the welding torch should be in a slightly uphill welding position. This facilitates penetration. Thick wall tube bottom welded. Wire cannot be added. However, the welding wire shall be added in the subsequent welding layer.
Related News

Telephone:+86-18594983359
E-mail:Firmkim@cn-huaguang.com
Zip Code: 311112
Address: No. 82, Qihang Road, Renhe Street, Yuhang District, Hangzhou City, Zhejiang Province

Douyin QR code

We chat number

WeChat public account